Applications that seem mechanically simple often combine startup peaks, position demands and restrictive packaging. The example is a 3D printer filament handling or auxiliary axis, with the specific goal to evaluate compact geared DC actuation without assuming it replaces every stepper. This makes filament feed speed, nip force and restart repeatability especially relevant. We examine mechanical load, electrical control and measurable acceptance evidence while guarding against the case where feed force stability and reaction time are ignored.
01. Identify the mechanism before the motor
A filament feeder, spool drive and enclosure actuator have different control and backdrive requirements, even within one printer. The first calculation belongs to the machine rather than the motor. On the 3D printer filament handling or auxiliary axis, locate the output load and describe its path through the coupling or shaft. Take account of startup and stopping as separate events. Then prepare a requirement sheet that explains what it means to evaluate compact geared DC actuation without assuming it replaces every stepper; keep assumptions distinct from measured mechanical demands.
02. Relate feeder force to roller torque
Drive wheel radius and traction determine how torque becomes filament force; slippage changes the relationship under jammed conditions. Set up one repeatable operating point on the 3D printer filament handling or auxiliary axis. Record the applied load and supply conditions, then collect load torque, support reaction and operating speed. The practical measurement method is a torque instrument or a documented force-and-radius calculation; retain a trace rather than only a pass/fail statement. This distinguishes a controller limit from resistance in the attached mechanism and makes later comparisons between candidates meaningful.
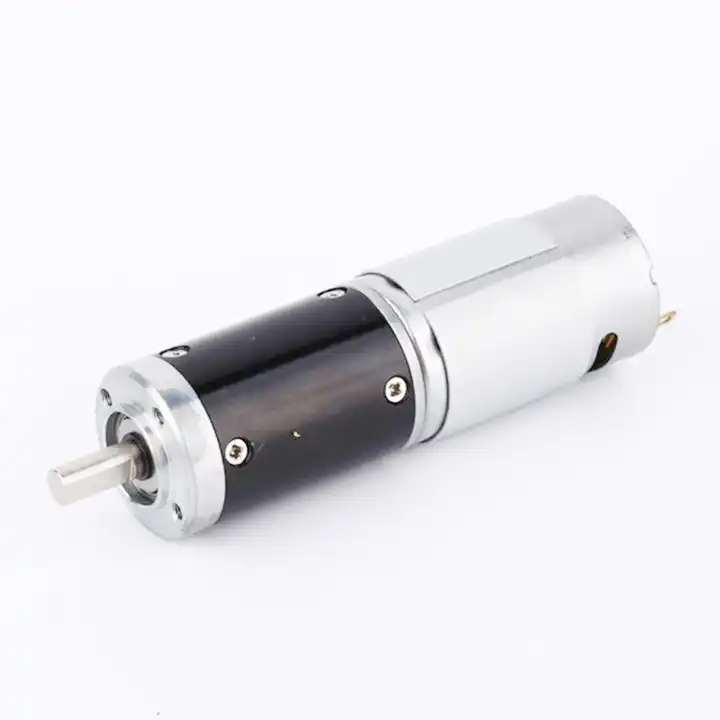
03. Evaluate positioning and metering needs
Precise extrusion may require synchronized position control, making feedback architecture as important as available torque. Use the measured output of the 3D printer filament handling or auxiliary axis to challenge the proposed drive choice. Calculate the needed motion, account for efficiency where specified and check the physical shaft reaction. The objective to evaluate compact geared DC actuation without assuming it replaces every stepper can be achieved only if the motor, reduction unit and controller each remain inside their individual ratings. Confirm those boundaries using functional extrusion/feed test under real material conditions.
04. Consider jam protection
A jam can hold the geared motor against a hard load; current or force limits should interrupt the drive before thermal damage. Assess transient loading on the 3D printer filament handling or auxiliary axis independently from the steady load. Momentum, breakaway friction and drive commands may create short peaks whose frequency determines the resulting heat and fatigue. The hazard to check is that feed force stability and reaction time are ignored. Set current limits and stopping rules before any representative overload investigation.
05. Review hot-enclosure conditions
Temperature near print chambers can affect the motor, lubrication and plastic attachments; verify component thermal ratings. The 3D printer filament handling or auxiliary axis can impose forces that a free gearmotor does not experience. Check the position of external supports, the coupling type and the path taken by mechanical reactions. Also look at cable routing through the intended motion range. A repeatable change after installation points toward a machine-interface issue that needs resolving at its source.

The design topic Review hot-enclosure conditions also raises a question about the reduction unit used with the 3D printer filament handling or auxiliary axis. For an overview of alternative arrangements, explore industrial planetary gear reduction. Reducer-only information must still be checked against the motor, driver and exact gearbox configuration considered for this application.
06. Plan packaging around service access
Filament cleaning, gear inspection and replacement should not require disturbing critical printer alignment. The test record should explain what was connected and what was commanded on the 3D printer filament handling or auxiliary axis. Instrument cycle duration, case temperature and surrounding air temperature using a repeatable duty-cycle test with temperature logging, then compare repeated trials at equivalent load and environmental conditions. If the reading drifts, investigate heat, drag and controller settings before selecting a replacement component. A reproducible result is worth more than an optimistic peak figure.
07. Compare alternatives by task
A stepper may be simpler for deterministic steps, while a DC gearmotor may suit an auxiliary movement with suitable feedback. The troubleshooting path for the 3D printer filament handling or auxiliary axis starts with the observation, not the part number. If an undocumented assumption at the mechanical interface is present, compare results before and after mechanical connection, provided that can be done safely. Recheck supply voltage and control commands, then investigate external load. Record which experiment changed the symptom and why.
- Confirm the measurement basis for compare alternatives by task, including instrument location and units.
- Record the normal and limiting operating states of the 3D printer filament handling or auxiliary axis.
- Compare the observed filament feed speed, nip force and restart repeatability with verified assembly documentation before approving this configuration.
08. Run a real print-cycle qualification
Observe feeding during starts, retractions and varied material friction; log dimensional consistency and motor current. Finish with a decision that can be checked on the 3D printer filament handling or auxiliary axis. The selected assembly must evaluate compact geared DC actuation without assuming it replaces every stepper with the intended supply, installed load and duty pattern. Keep the approved interface drawing and functional extrusion/feed test under real material conditions alongside the test results. If a future machine revision alters those conditions, requalify the motor-and-reducer combination rather than assuming the earlier approval still applies.
09. Numerical screening for 3D printer filament handling or auxiliary axis
For illustration, imagine the 3D printer filament handling or auxiliary axis under its design load. Imagine the selected mechanism repeats a four-second movement followed by a six-second dwell. A basic test can log output displacement, peak current and housing temperature for each ten-second cycle. This example defines a test method, not a product performance claim. The important conclusion is not one output number but which portion of filament feed speed, nip force and restart repeatability has been measured. Test the resulting drive against functional extrusion/feed test under real material conditions when aiming to evaluate compact geared DC actuation without assuming it replaces every stepper.
10. Verification procedure: filament feed speed, nip force and restart repeatability
Build a controlled test around 3D printer filament handling or auxiliary axis. Inspect the shaft, pilot and electrical leads before coupling the load, and log filament feed speed, nip force and restart repeatability during the operating event. With the final mechanism attached, compare results with functional extrusion/feed test under real material conditions. An indication that feed force stability and reaction time are ignored calls for stopping the trial and identifying which component sets the limit.
| Engineering checkpoint | Observation for 3D printer filament handling or auxiliary axis | Approval implication |
|---|---|---|
| Machine duty | filament feed speed, nip force and restart repeatability | Keep the measured conditions of 3D printer filament handling or auxiliary axis comparable |
| Output interface | Mounting and wiring of the 3D printer filament handling or auxiliary axis | Check review hot-enclosure conditions against the drawing |
| Evidence basis | functional extrusion/feed test under real material conditions | Confirms evaluate compact geared DC actuation without assuming it replaces every stepper |
| Escalation trigger | feed force stability and reaction time are ignored | Stop for review if the 3D printer filament handling or auxiliary axis behaves outside limits |
11. What to specify when quoting this application task
A comparable quote for 3D printer filament handling or auxiliary axis requires more than voltage and nominal ratio. Provide the physical interface drawing, motion duty and the measurable target: evaluate compact geared DC actuation without assuming it replaces every stepper. Ask each supplier to respond to filament feed speed, nip force and restart repeatability and identify the exact test or catalogue basis for functional extrusion/feed test under real material conditions.
- State the device and target: 3D printer filament handling or auxiliary axis; evaluate compact geared DC actuation without assuming it replaces every stepper.
- Include locating pilot, shaft and flange tolerances for the 3D printer filament handling or auxiliary axis installation.
- Identify voltage and feedback needed for the 3D printer filament handling or auxiliary axis, including motor-driver protections.
- Connect filament feed speed, nip force and restart repeatability to peak and continuous load cases and relevant cycle timing.
- Record installation constraints for the 3D printer filament handling or auxiliary axis and the planned acceptance method.
- Confirm functional extrusion/feed test under real material conditions before release of the exact motor-reducer option.
12. Release decision for 3D printer filament handling or auxiliary axis
Maintain a short history of accepted and rejected drive arrangements for 3D printer filament handling or auxiliary axis. File measured filament feed speed, nip force and restart repeatability beside functional extrusion/feed test under real material conditions; include the reason a candidate could or could not evaluate compact geared DC actuation without assuming it replaces every stepper. This makes the failure scenario that feed force stability and reaction time are ignored visible when later production batches arrive.
Questions raised by 3D printer filament handling or auxiliary axis applications
Why is identify the mechanism before the motor important for this application?
A filament feeder, spool drive and enclosure actuator have different control and backdrive requirements, even within one printer. In the 3D printer filament handling or auxiliary axis, the review should link that condition to filament feed speed, nip force and restart repeatability before a motor is selected.
What mistake should be avoided when considering consider jam protection?
A jam can hold the geared motor against a hard load; current or force limits should interrupt the drive before thermal damage. A failure to document the issue may lead to the situation where feed force stability and reaction time are ignored.
How should compare alternatives by task be checked?
A stepper may be simpler for deterministic steps, while a DC gearmotor may suit an auxiliary movement with suitable feedback. Collect evidence during the intended movement of the 3D printer filament handling or auxiliary axis, not only while the output runs freely.
What records verify the 3D printer filament handling or auxiliary axis drive configuration?
Provide the machine drawing, motor control requirements, filament feed speed, nip force and restart repeatability and functional extrusion/feed test under real material conditions. Explain the application goal: evaluate compact geared DC actuation without assuming it replaces every stepper.
To discuss evaluate compact geared DC actuation without assuming it replaces every stepper on a 3D printer filament handling or auxiliary axis, send the measurement summary and interface drawing to продажі@planetarymotors.top. Include the filament feed speed, nip force and restart repeatability so the motor and reduction unit can be assessed together.